Choosing the best China Zero Leakage Butterfly Valve manufacturer requires more than comparing prices or polished brochures. A dependable supplier must prove sealing performance under real operating conditions. Look for documented pressure tests, material traceability, cycle testing, and consistent inspection records. The valve should close firmly, without damaging its resilient seat or shaft seal.
Valve engineering specialist David W. Smith states, “Zero leakage is not a promise on paper; it is a result measured at the seat.” This principle deserves attention. However, the quotation should be verified against an original publication before formal use. That small imperfection matters. Trust should not depend on attractive wording.
In practical evaluation, inspect the valve body, disc edge, seat geometry, and actuator response. Ask how each unit is tested before shipment. A serious manufacturer can explain testing standards, coating thickness, temperature limits, and replacement procedures clearly. It should also provide drawings, certificates, and application references.
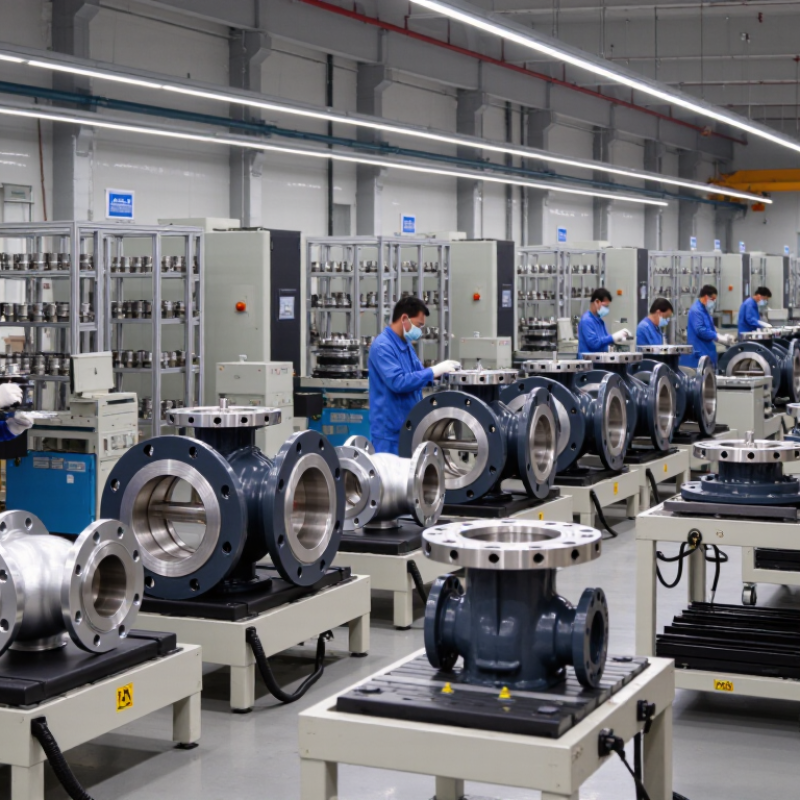
China has many capable valve producers, but capability varies widely. Some factories offer excellent machining and disciplined assembly. Others rely heavily on generic components and broad performance claims. A careful buyer should compare evidence, not assumptions. Site audits can reveal details that catalogs hide, including cleanliness, calibration habits, storage conditions, and operator training.
This guide examines how to identify the best China Zero Leakage Butterfly Valve manufacturer. It considers engineering quality, manufacturing experience, after-sales support, and long-term reliability. No single checklist is perfect. Field conditions can expose weaknesses that laboratory testing misses. That is why honest evaluation remains essential.
A zero-leakage butterfly valve is designed to stop visible fluid passage when fully closed. In engineering practice, “zero leakage” usually means no detectable leakage under a defined test standard and pressure. It does not promise perfect sealing forever. Seal condition depends on temperature, pressure, media, installation, and service time.
The valve uses a circular disc mounted inside the pipeline. A quarter-turn actuator rotates the disc from open to closed. As the disc reaches its seat, the sealing surface creates continuous contact around the flow passage. Soft seats can provide tight shutoff with resilient contact. Metal-seated designs suit higher temperatures and abrasive duties, but their sealing accuracy demands stricter machining. Double-offset or triple-offset structures reduce rubbing during rotation. This lowers wear and operating torque.
Reliable performance starts with correct sizing. An oversized valve may operate near its closed position, making control unstable. Dirty fluid can also damage the seat. Small particles matter. During inspection, technicians should check flange alignment, stem movement, seat condition, and actuator torque. Pressure testing should follow a recognized procedure, such as ISO 5208 or API 598, when applicable. Field conditions are often less tidy than workshop tests. A valve may pass inspection yet leak later because of thermal cycling, pipe stress, or incorrect installation. That uncomfortable detail deserves attention. Selecting materials only from a catalog is not enough; actual pressure, temperature, fluid chemistry, and maintenance access must guide the decision.
China Best Zero Leakage Butterfly Valve Manufacturer?
A zero-leakage claim needs careful testing. No valve seals perfectly under every temperature, pressure, or cycle. The better target is near-zero leakage under defined conditions. ISO 5208 and API 598 provide recognized pressure-testing methods for industrial valves. They also distinguish acceptable leakage classes.
A resilient seat must press evenly against the disc edge. A precision-machined disc reduces scratches and uneven contact. Double-offset or triple-offset designs can lower seat friction during opening. This helps prevent early wear. Stem sealing also matters. A multi-layer packing system, controlled compression, and an anti-blowout stem reduce external leakage. According to the U.S. EPA’s Leak Detection and Repair guidance, valves are often the largest group of leaking components in process facilities, commonly reported near 60%. IEA’s Global Methane Tracker 2024 estimated about 120 million tonnes of methane emissions from oil and gas operations in 2023. These figures make sealing quality an operating issue, not merely a purchasing detail.
Tips: Check the leakage standard, pressure class, temperature range, and test medium. Ask for test records, not only certificates. Inspect the seat after repeated cycling. Small defects matter. Field alignment is easy to underestimate. Even a well-designed valve may leak when pipelines impose stress or the actuator is poorly adjusted. This deserves reflection.
Typical sealing barriers used in resilient-seated butterfly valve designs
A zero-leakage design relies on multiple sealing interfaces rather than a single component. Typical barriers include dual stem sealing, elastic seat-to-disc contact, body-to-seat sealing, and flange gaskets. The exact arrangement varies by valve size, pressure class, temperature, and applicable testing standard.
China Best Zero Leakage Butterfly Valve Manufacturer?
Materials, standards, and testing decide whether “zero leakage” is credible. The World Bank’s widely cited utility assessments report water losses reaching 30% in some distribution systems. A poorly selected valve can worsen these losses through seat damage, shaft wear, or uneven installation. For clean water, ductile iron bodies with fusion-bonded epoxy coatings are common. Stainless steel trim suits corrosive fluids. EPDM seats handle water well, while NBR supports many oil-related applications. Material compatibility must be checked against temperature, pressure, and fluid chemistry.
Standards provide measurable boundaries. ISO 5208 and EN 12266-1 define pressure testing and leakage classes, including Rate A, which requires no visible leakage during the test. API 609 addresses butterfly valve design and pressure-temperature considerations. AWWA C504 remains relevant for rubber-seated valves in waterworks service. These documents do not replace engineering judgment. They establish test conditions.
A reliable manufacturer should record shell tests, seat tests, torque readings, and coating thickness. It should also provide traceability for castings, elastomers, and inspection results. In practical testing, a valve may pass at room temperature yet perform differently after thermal cycling. That detail is easy to miss. I would question any “zero leakage” claim without the test medium, pressure, duration, and acceptance standard. Installation matters too. Misaligned piping can overload the disc and shorten seat life. Perfect sealing is a target, not a slogan.
The search for a China-based butterfly valve manufacturer should begin with evidence, not impressive claims. Zero leakage sounds absolute. In practice, performance depends on valve design, seat material, pressure, temperature, and installation quality. Ask whether the manufacturer follows recognized testing standards, such as API 598 or ISO 5208. Request recent test records for the same valve design, size, and pressure class.
Examine material traceability from casting to final assembly. Body certificates, shaft specifications, seat compound, and coating records should match the purchase documents. A reliable factory can explain its machining tolerances, sealing method, and inspection checkpoints clearly. It should also provide hydrostatic and seat leakage results with identifiable serial numbers. Avoid accepting generic certificates.
Factory experience matters beyond equipment. Review export history, engineering support, spare-part availability, and response procedures for failures. Ask for photographs of production stages, not only a showroom tour. A polished factory tour can still hide weak documentation. I would also arrange an independent pre-shipment inspection for critical orders. This adds cost, but it may reveal damaged seats, uneven coatings, or incorrect markings. Do not judge quality by price alone. Cheap valves can become expensive during shutdowns. Even a careful evaluation has limits; field installation, storage, and operator practices can still affect leakage performance.
China Best Zero Leakage Butterfly Valve Manufacturer?
Manufacturing quality starts with design control, not polished paint. A reliable factory should control body casting, disc alignment, stem fit, and seat compression. ISO 5208 defines leakage grades, while Rate A requires no visible leakage during the specified test. “Zero leakage” should mean zero detectable leakage under defined conditions, not an unlimited promise.
Testing must be traceable. API 598 requires shell and closure testing for industrial valves, with pressure, duration, and acceptance criteria recorded. Ask for serial-numbered test reports, calibrated gauges, and pressure charts. Inspectors should verify every lot, not only attractive samples. A practical audit checks dimensional records, material certificates, coating thickness, and repeated opening cycles. Small details matter.
Supplier verification needs evidence. Request recent third-party inspection records and compare them with factory test data. Confirm whether tests use clean water, the correct pressure, and a stable temperature. ISO 9001 certification supports process control, but it does not prove zero leakage by itself. That distinction is often missed. Site visits can reveal rushed assembly, mixed seals, or gauges past calibration. I would also test a random production valve independently. It costs more. Still, one failed valve in a critical pipeline can cost far more. Some suppliers provide excellent documents but inconsistent batches, so verification should continue after the first order.
| Evaluation Dimension | Manufacturing or Testing Requirement | Recommended Benchmark | Verification Evidence |
|---|---|---|---|
| Valve Design | Concentric, double-eccentric, or triple-eccentric butterfly valve design should be clearly identified, including the sealing mechanism and intended service conditions. | The design type, pressure class, temperature range, flow direction, and installation orientation are documented before quotation. | Approved drawings, sectional drawings, technical data sheets, and design calculation records. |
| Applicable Product Standard | The valve design and construction should follow a recognized butterfly valve standard suitable for the application. | Common references include EN 593, API 609, or another contractually specified equivalent standard. | Certificate of conformity, controlled product specification, and a clause-by-clause compliance statement. |
| Body and Disc Materials | Pressure-retaining and wetted materials must match the fluid, temperature, pressure, and corrosion conditions. | Material grades are stated on drawings and purchase documents; heat numbers are traceable to mill certificates. | Material test certificates, positive material identification records where required, and heat-number traceability. |
| Seat Material Selection | Seat material must be compatible with the medium, operating temperature, pressure differential, and cycle frequency. | Soft seats may provide bubble-tight shutoff within their rated limits; metal-seated designs require application-specific leakage acceptance. | Seat material specification, temperature limits, chemical compatibility data, and approved material certificates. |
| Machining Accuracy | Disc, shaft, body bore, seat-retaining surfaces, and flange interfaces should be machined to controlled tolerances. | Critical dimensions and tolerances are defined on controlled drawings and checked with calibrated instruments. | In-process inspection reports, dimensional records, calibration certificates, and nonconformance reports. |
| Pressure Boundary Test | The valve body and pressure-retaining components should be hydrostatically tested for structural integrity. | Testing is performed according to the purchase specification and a recognized test standard such as API 598 or ISO 5208. | Valve-specific pressure test report showing test medium, pressure, duration, temperature, gauge identification, and result. |
| Seat Leakage Test | The closed valve should be tested in the specified flow direction or both directions when required by the design and contract. | Acceptance is defined by the selected leakage class or rate in ISO 5208, EN 12266-1, API 598, or the project specification. | Recorded leakage rate, test pressure, stabilization time, test direction, seat condition, and authorized inspector signature. |
| Zero-Leakage Claim | “Zero leakage” should be treated as a defined test result rather than an unlimited operating guarantee. | The supplier states the applicable test standard, leakage class, pressure range, temperature, medium, and test duration. | Written leakage definition, witnessed test record, and contractually agreed acceptance criteria. |
| Operating Torque | Breakaway, running, and seating torque should be measured or calculated for the complete valve assembly. | Actuator sizing includes maximum differential pressure, seat friction, safety factor, and service temperature. | Torque calculation, test curve, actuator sizing sheet, and manual or automated operation record. |
| Shaft and Anti-Blowout Construction | The shaft connection and retention system should prevent unintended shaft displacement during operation or maintenance. | The design includes documented shaft retention and, where applicable, anti-blowout features. | Assembly drawing, design-risk review, inspection checklist, and functional operating test. |
| Flange and Face-to-Face Dimensions | Connection dimensions must match the piping system and the specified valve dimensional standard. | Face-to-face dimensions and flange drilling comply with the applicable standard or approved project drawing. | Dimensional inspection report, calibrated measuring equipment record, and final drawing approval. |
| Surface Protection | External coating, internal lining, or corrosion protection should be suitable for storage, transport, and service exposure. | Coating system, surface preparation, dry-film thickness, curing conditions, and repair procedure are specified. | Coating inspection report, dry-film thickness readings, surface-preparation record, and coating batch information. |
| Assembly Cleanliness | Valve internals should be free from machining chips, abrasive residue, welding debris, grease contamination, and foreign matter. | Cleaning and preservation procedures are defined according to the service, especially for oxygen, potable water, or hygienic applications. | Cleaning checklist, visual inspection record, preservation statement, and packing inspection photographs. |
| Actuator and Accessory Compatibility | Manual gearboxes, pneumatic actuators, electric actuators, limit switches, solenoid valves, and positioners must match the valve interface and torque requirement. | Valve mounting dimensions comply with ISO 5211 where applicable, and the complete assembly is function-tested. | Interface drawing, actuator data sheet, open-close cycle test, switch-setting record, and fail-position confirmation. |
| Production Traceability | Each valve should be traceable from raw material through machining, assembly, testing, marking, and shipment. | A unique serial number links the valve to material certificates, inspection records, test results, and final release documents. | Manufacturing record book, serial-number register, heat-number log, and final data-book index. |
| Quality Management System | The manufacturing facility should operate a documented quality management system with controlled procedures and corrective actions. | A current ISO 9001 certificate is verified against the issuing certification body and the actual manufacturing site. | Valid certificate, certification scope, latest surveillance status, internal audit records, and corrective-action samples. |
| Calibration Control | Pressure gauges, torque meters, dimensional tools, coating gauges, and electrical test instruments must be calibrated. | Calibration is current, traceable to recognized national or international measurement standards, and suitable for the required accuracy. | Calibration certificates, instrument register, due-date labels, and out-of-tolerance handling procedure. |
| Third-Party Inspection | Independent inspection may be used for material review, dimensional checks, pressure testing, coating inspection, and final release. | Inspection and Test Plans define hold points, witness points, document review, and rejection criteria before production begins. | Approved ITP, inspector qualifications, signed inspection reports, and release certificate. |
| Supplier Factory Audit | The buyer should verify manufacturing capacity, subcontractor control, testing facilities, warehouse conditions, and document management. | The audit covers actual production capability rather than only trading or office operations. | Audit checklist, production-line photographs, equipment list, employee competency records, and closed audit findings. |
| Sample Validation | Pre-production or production samples should be inspected and tested against the approved specification before volume shipment. | Sample approval includes dimensions, materials, operation, pressure boundary integrity, seat leakage, coating, and marking. | Approved sample report, signed inspection checklist, test certificates, and comparison against the purchase order. |
| Final Documentation | The final document package should be complete, consistent, and linked to each valve serial number. | The package includes drawings, material certificates, pressure and leakage test reports, inspection records, certificates, and operating instructions. | Indexed manufacturing data book, document-review checklist, and buyer-approved final release package. |
| Warranty and After-Sales Support | The supplier should define warranty coverage, exclusions, spare-parts availability, technical response time, and claim investigation procedures. | Warranty terms are written into the contract and supported by identifiable service contacts and replacement-part data. | Warranty certificate, spare-parts list, maintenance instructions, response procedure, and previous corrective-action examples. |